Skip to content

The test has been conducted. Providing proof should not be the problem.

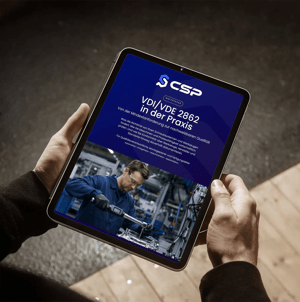
15 pages of plain language explaining how to correctly classify every bolted joint, justify risk-based intervals for MFU and PFU, and demonstrate compliance across tools, manufacturers, and locations—even for production lots from seven years ago.

✓ Risk assessment for each fastening point, from Category A to C
✓ MFU and PFU: Set intervals and justify them during the audit
✓ Checklist with seven questions for self-assessment

For quality managers, assembly planners, and production managers
: Automotive · Plant Engineering · Mechanical Engineering · Equipment Manufacturing
whitepaper-vdivde-2862

THE MOMENT

The auditor is asking about Station 14. You have two minutes.

The inspection was performed. Everyone in the room knows that. The only question is where the documentation is: in the screwdriver’s manufacturer software, in a spreadsheet on the maintenance department’s drive, or in a folder maintained by the colleague who left last year.

This is precisely where it is determined whether you can demonstrate due care or merely claim to have exercised it. Case law requires manufacturers to operate in accordance with the recognized state of the art. For screw assembly in general industry, this standard has been defined by VDI/VDE 2862 Part 2 since February 2015.

whitepaper-vdivde-2862
CONTENTS

What’s in the White Paper

From risk assessment of individual bolted joints to MFU and PFU, all the way to documentation that remains valid even years later. Not a product brochure, but a working guide.

The Legal Framework

Why a non-statutory guideline becomes the standard in the event of damages.

The Three Categories of Fastening Applications

How to evaluate each bolted joint and what minimum requirements result from this.

From Category to Tool

Two questions determine the tool class and the testing effort. Both are covered in the white paper.

MFU and PFU at a Glance

What these two inspections entail, what inspection intervals have become standard practice, and how to justify a deviation.

The Typical Gaps

Why testing organizations fail in practice—from siloed solutions to vendor lock-in.

Checklist and Steps to Follow

Seven questions for a self-assessment. If you can’t answer any of them, you’ll know where to start.

Request a white paper

PDF, 15 pages. Delivered immediately by email.

THE CLASSIFICATION

Every bolted joint carries a risk. The classification determines the effort required and liability.

Classifying a risk too low jeopardizes safety. Classifying it too high costs money that could be better spent elsewhere. Here is the logic you should use to make your decision.

CATEGORYA

High Risk: Danger to life, limb, or the environment

Improper screw connections must be reliably detected—control and monitoring parameters, all screw data documented.


TYPICAL TOOL CLASS

Measuring and monitoring fastening system with data logging

CATEGORYB

Medium Risk: Malfunction or Equipment Shutdown

Compliance with the specification must be ensured, ideally through counting and a group signal.


TYPICAL TOOL CLASS

Shut-off tool with counting and signaling functions

CATEGORYC

Low risk: non-critical

It must be possible to reliably apply the specified torque.


TYPICAL TOOL CLASS

Tool with precisely adjustable torque

Get the white paper, and then sign up for your live demo.

In 30 minutes, we’ll use your own screwdriving scenarios to show you what compliance-compliant documentation looks like in practice—specifically, using your data.

35+

Years of shop floor experience

200+

Facilities worldwide in full-scale operation

4

Software Solutions as a Closed-Loop Platform

1

Mission: Turning Data into Impact